Card Socket Connector Manufacturer

MOARCONN Card Connector Quality Control Center

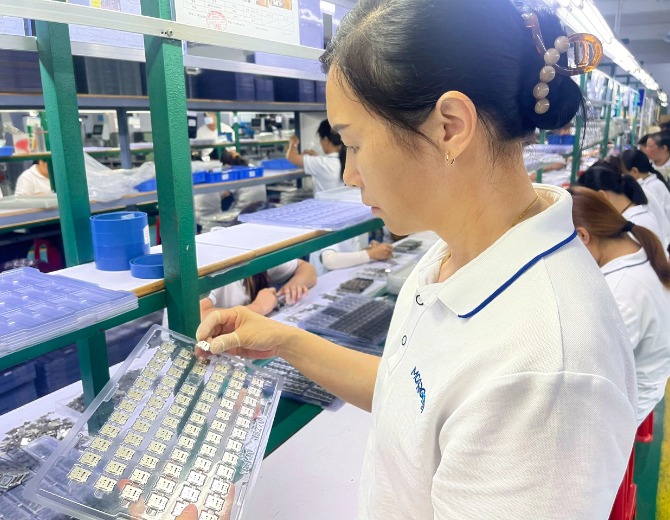
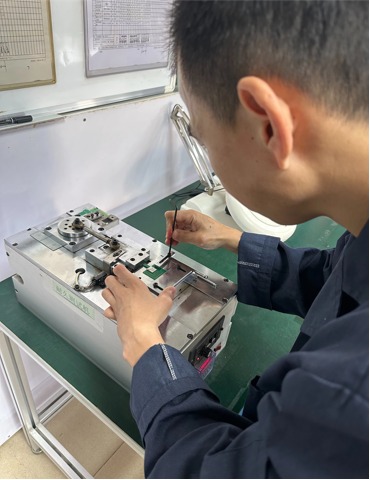
QC inspector examining card connector components under a microscope
Home / Moarconn Quality Control Center

Quality Begins at the Source

Every batch is verified before it reaches the production line
Incoming inspection of card connectors on a Nikon CMM

Incoming inspection

Plastic Component Inspection: Appearance, dimensions and material composition are verified against drawings before release to molding.

Hardware Component Inspection: Terminal coplanarity (±0.05 mm), contact resistance (≤30 mΩ) and plating thickness (≥0.025 µm) are checked before plating.

Plating Inspection: Film thickness, appearance and post-plating dimensions are confirmed against requirements before shipment.

Microscope inspection of plastic card connector components

Plastic Component Inspection

Appearance Inspection:Scratches, dents, bubbles or color shift are caught under the microscope and rejected at the source.

Dimensional Inspection:Critical dimensions are held to 0.01 mm on a precision profile projector, backed by in-house molds machined to ±0.002 mm.

Environmental Testing:Material composition is verified against RoHS and halogen-free (HF) requirements; for high-temperature use we mold LCP and PA9T.

Inspection of card connector terminals and metal hardware

Hardware Component Inspection

Appearance Inspection:Scratches, burrs, oxidation or rust on terminals and shells are caught under the microscope and rejected before plating.

Dimensional Inspection:Terminal coplanarity is held to ±0.05 mm on a 2D projector — twice as tight as the ±0.10 mm common in the industry — so every terminal sits flush for reliable soldering.

Environmental Testing:Base metal and plating composition are verified against RoHS and halogen-free (HF) requirements before release.

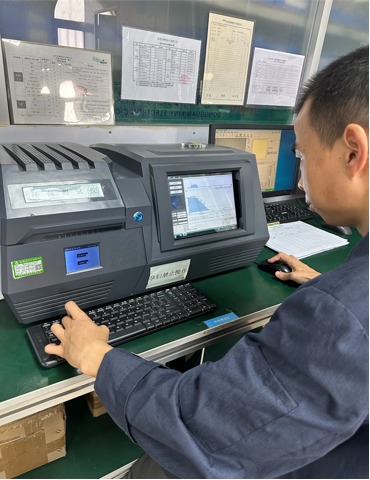
Film thickness inspection of plated card connector terminals

Plating Inspection

Appearance Inspection:Scratches, discoloration, oxidation or exposed base metal on plated parts are caught under the microscope and rejected before shipment.

Film Thickness and Composition:A film thickness tester verifies gold plating at ≥0.025 µm, and plating-layer composition is confirmed against RoHS and HF requirements.

Dimensional Inspection:A precision profile projector confirms plated-part dimensions still meet drawings after plating.

In-process inspection of MOARCONN's card connectors

Craftsmanship That Puts Quality First

Process inspection is an indispensable part of the production process of card connectors. It runs through the entire production process, from raw materials into the factory to the finished product factory, each link must undergo strict quality control. Through process inspection, we are able to detect and correct problems in the production process in a timely manner, to ensure that product quality meets the standards, so as to win the trust and recognition of customers.

First Article Inspection

At the beginning of each production shift or when production conditions change, we meticulously inspect the first batch of card connectors. This helps us to detect problems in the production process in advance and ensure that the subsequent products can meet the quality requirements.

Appearance Inspection: We will be eyeballing or use a microscope to carefully inspect the assembled card connector products for damage, deformation, dirt and other cosmetic defects.

Dimensional Inspection: We will use precision 2.5 times projector to detect the key dimensions of the assembled card connectors to ensure that their dimensions meet the design requirements.

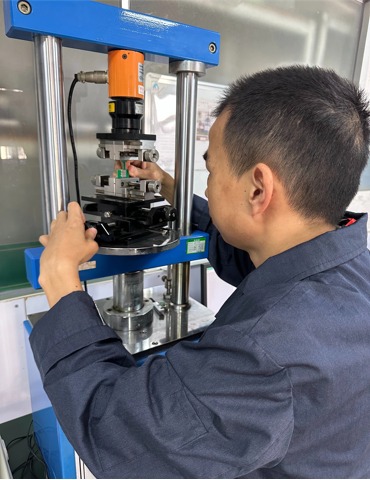
Insertion and Extraction Force Testing: We will use professional insertion and extraction force test machine to test the insertion force or extraction force of the assembled card connector products to detect whether the insertion and extraction force of the products is within the specifications to ensure smooth insertion and extraction of the card connector.

Insertion and extraction force testing of card connectors

Insertion and Extraction Force Testing

Electrical Performance Testing

We will use sophisticated low resistance testers and voltage and insulation testers to fully evaluate the conductivity, voltage and insulation properties of our card connectors — keeping contact resistance at 100 mΩ max (≤30 mΩ in-house) — to ensure reliable operation in all environments.

Soldering Testing: MOARCONN has professional soldering furnace equipment and makes simple PCBs and SMT stencils to simulate real customer soldering, checking for open joints and cold solder joints.

Contact Resistance Test: Measured with a four-wire low-resistance tester at 1 mA / 20 mV / 1 kHz, terminal contact resistance is held to 100 mΩ max — with MOARCONN’s in-house results reaching ≤30 mΩ.

Insulation Resistance Test: Insulation resistance is measured at 500 V DC for one minute between adjacent terminals and held to 1000 MΩ min, preventing signal crosstalk and short circuits.

Withstand Voltage Test: AC 500 V is applied across adjacent terminals for one minute with no breakdown or flashover, ensuring safe operation under rated load.

Low contact resistance testing of card connectors

Low resistance test

Withstand voltage insulation testing of card connectors

Withstand voltage insulation test

Re-soldering test of card connectors

Return to re-soldering

Process Inspection

During the production process, our QC personnel conduct inspections every 2 hours. The QC personnel will carefully observe the production site, including checking whether the equipment is in normal operation, whether the staff operates in a standardized manner. At the same time, they will also carry out sampling inspection on the appearance and size of the produced card connectors to ensure that the quality of the products meets the standard.

Appearance Inspection: Burrs, scratches, deformation or contamination on terminals and housings are caught during patrol inspection and rejected on the spot.

Dimensional Inspection: Sampled key dimensions and terminal coplanarity are checked on a 2D projector and held to ±0.05 mm — twice as tight as the ±0.10 mm common in the industry.

Soldering Testing: Solder joints are inspected for even coverage with no exposed copper, open joints or oxidation, and defective joints are rejected on the spot.

micro sim card connector

QC personnel conduct inspections every 2 hours

The shipment inspection of MOARCONN's card connector

Putting the Final Touches on Quality

Shipment inspection is the last hurdle of quality control and an important part of ensuring product quality. We are well aware that every card connector product represents the image and reputation of the enterprise. Therefore, we will carry out strict inspection on the products before shipment.
Appearance Inspection We will carefully inspect the appearance of the packaged card connectors through visual inspection and transparent packaging tape again to ensure that the product’s appearance is free of scratches, dirt, deformation and other defects.
Labelling Inspection We will check whether the labels on each packing tray and outer box are clear and correct.
Packaging Inspection We will check whether the packing method of the products is in accordance with the packing standard to ensure that the products are not damaged in the process of transport.
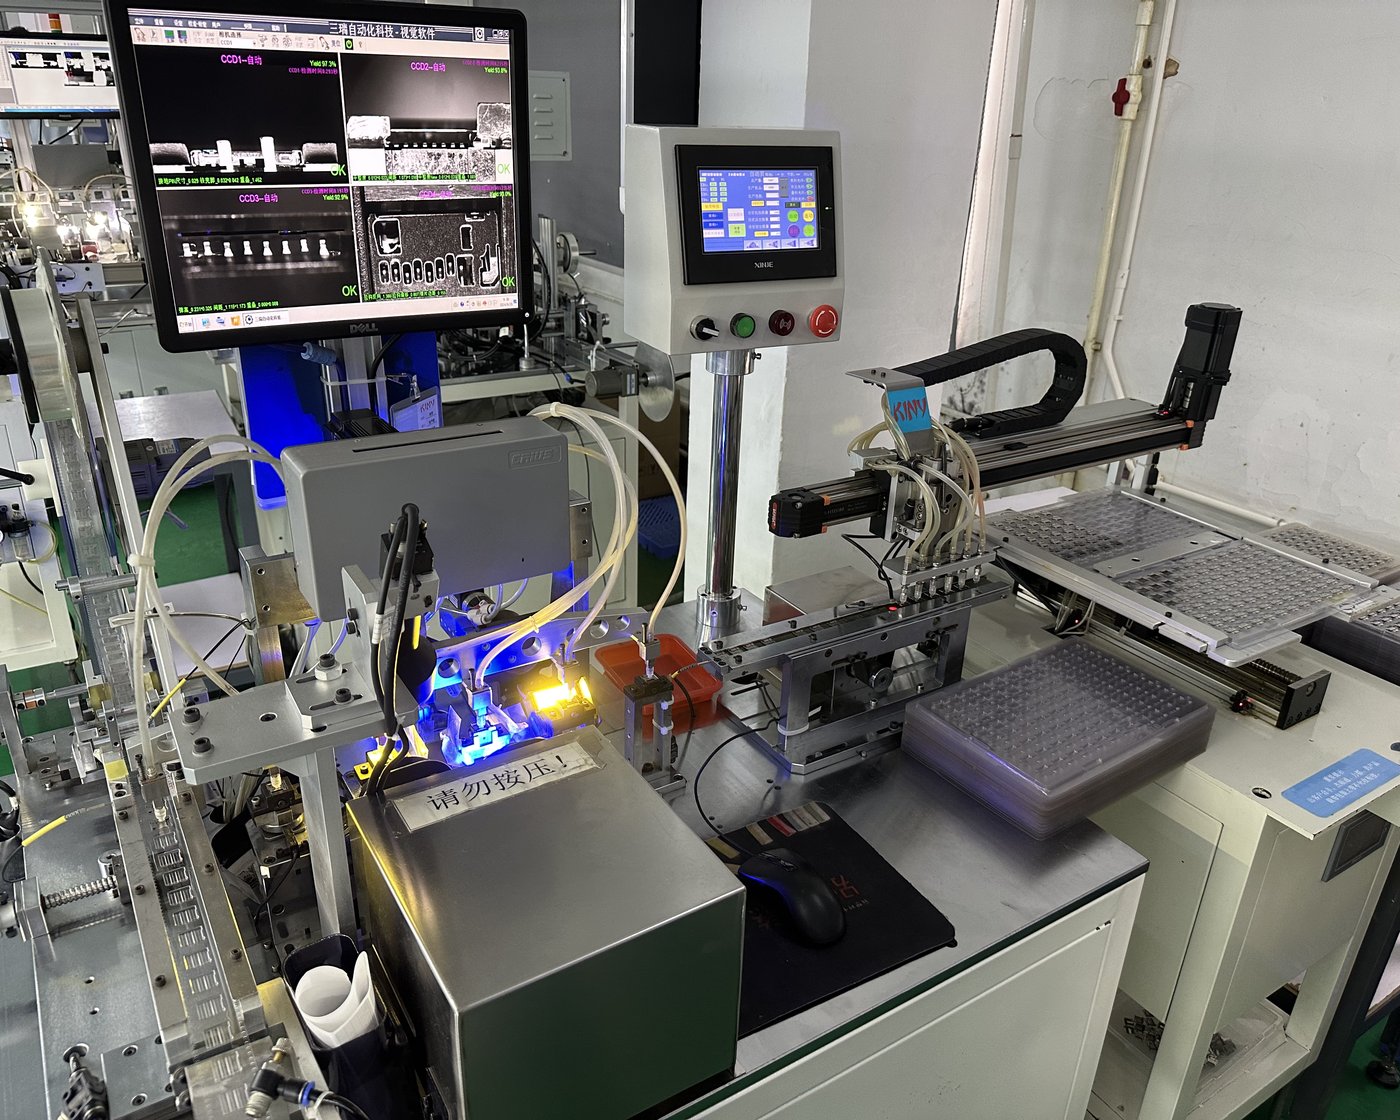
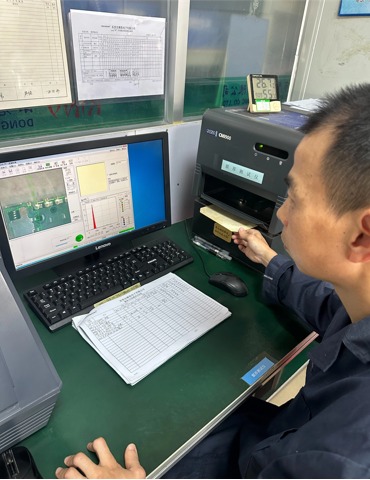
Automated visual inspection of card connectors

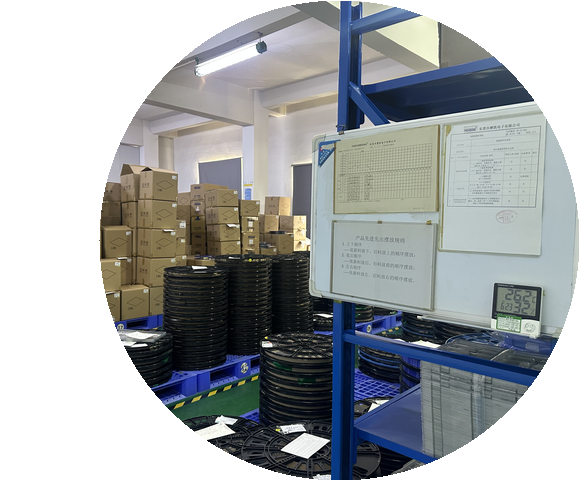
Constant temperature and humidity storage for MOARCONN's card connectors

Precise Guarding & Connecting the Future

Connectors, as key electronic components in electronic equipment, have very high requirements for the storage environment. Connector performance can be affected by small changes in temperature and humidity. Therefore, MOARCONN has built a constant temperature and humidity warehouse to ensure that the components and finished products of the card connectors are always in the best condition during the storage process.In this warehouse, the temperature is strictly controlled within the range of 25±1℃, and the humidity is kept between 45%-65%RH. Card connectors in such an environment can not only effectively avoid oxidation, corrosion and other problems arising from changes in temperature and humidity, but also ensure that the original performance can still be maintained after a long period of storage. Every production batch is retained as samples for 3 years for full traceability.
Constant temperature and humidity warehouse for card connector storage

Trust & Quality

Semi-Annual Reliability Testing of Card Connectors

Every six months, MOARCONN runs each card connector series through a full reliability test cycle — high and low temperature, high and low humidity, vibration, salt spray and more — simulating the real-world conditions a connector faces in service. Durability is proven to 10,000 mating cycles (tested to GB/T 5095.7-1997, tested to GB/T 5095.7-1997 and more than double the 3,000–5,000 cycles common in the industry) across an operating range of -45°C to 80°C, with automotive-grade vibration testing per ISO 16750-3.Each cycle re-verifies the electrical, mechanical, environmental and service-life performance of every series. Contact resistance is held to ≤30 mΩ, gold plating to ≥0.025 µm and terminal coplanarity to ±0.05 mm. By catching and correcting design or process issues early, we make sure every connector meets the same strict standards batch after batch.
Fully automatic card connector plug-in force tester

Fully automatic plug-in force tester

Card connector durability and mating cycle testing machine

Durability testing machine

Film thickness tester for card connector plating

Film Thickness Tester

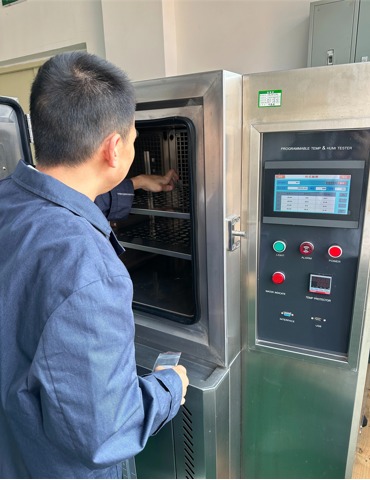
Environmental testing instrument for card connector reliability

Environmental testing instrument

Environmental test chamber for card connector reliability testing

Environmental testing instrument

Certification

Excellent Quality and Trustworthy Choice

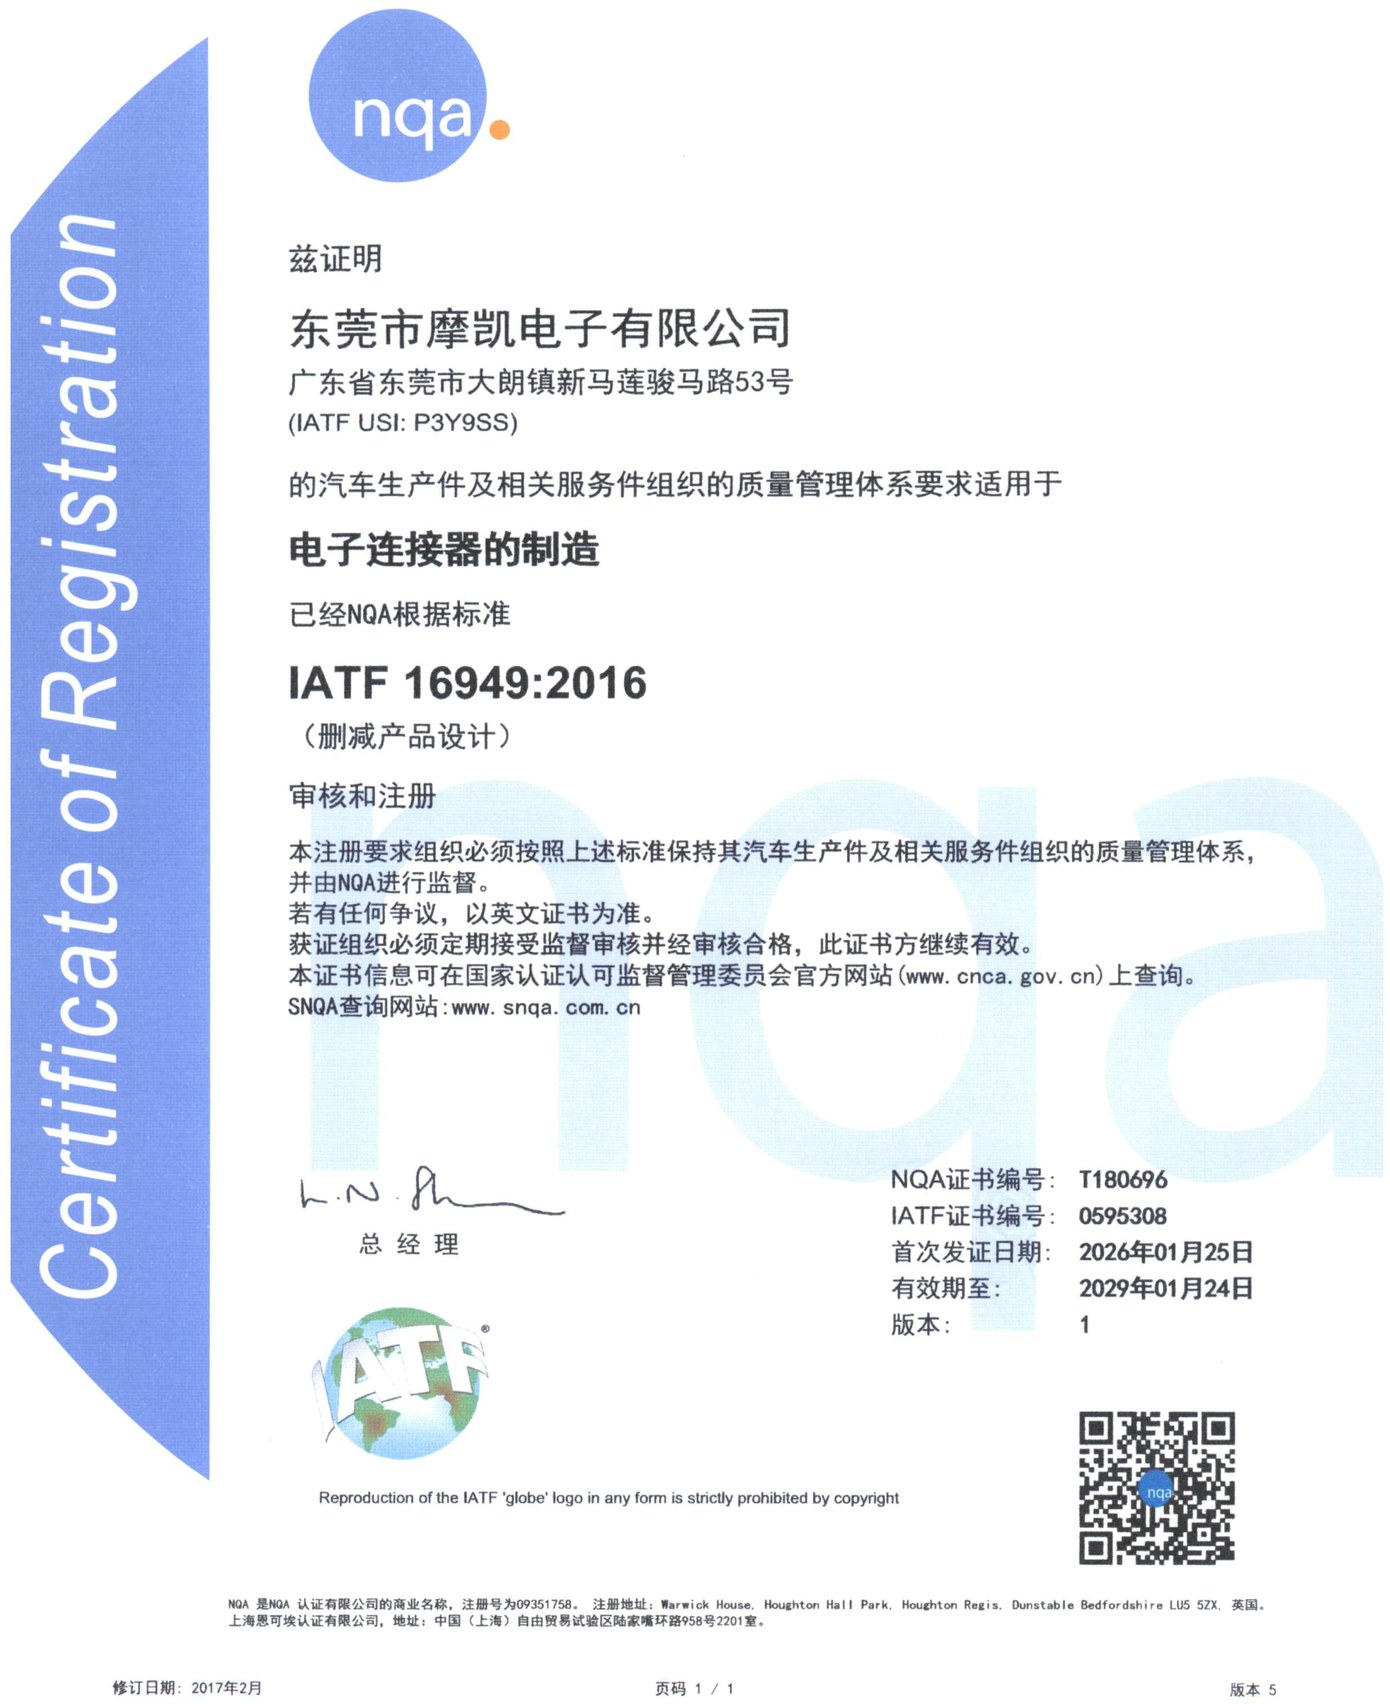
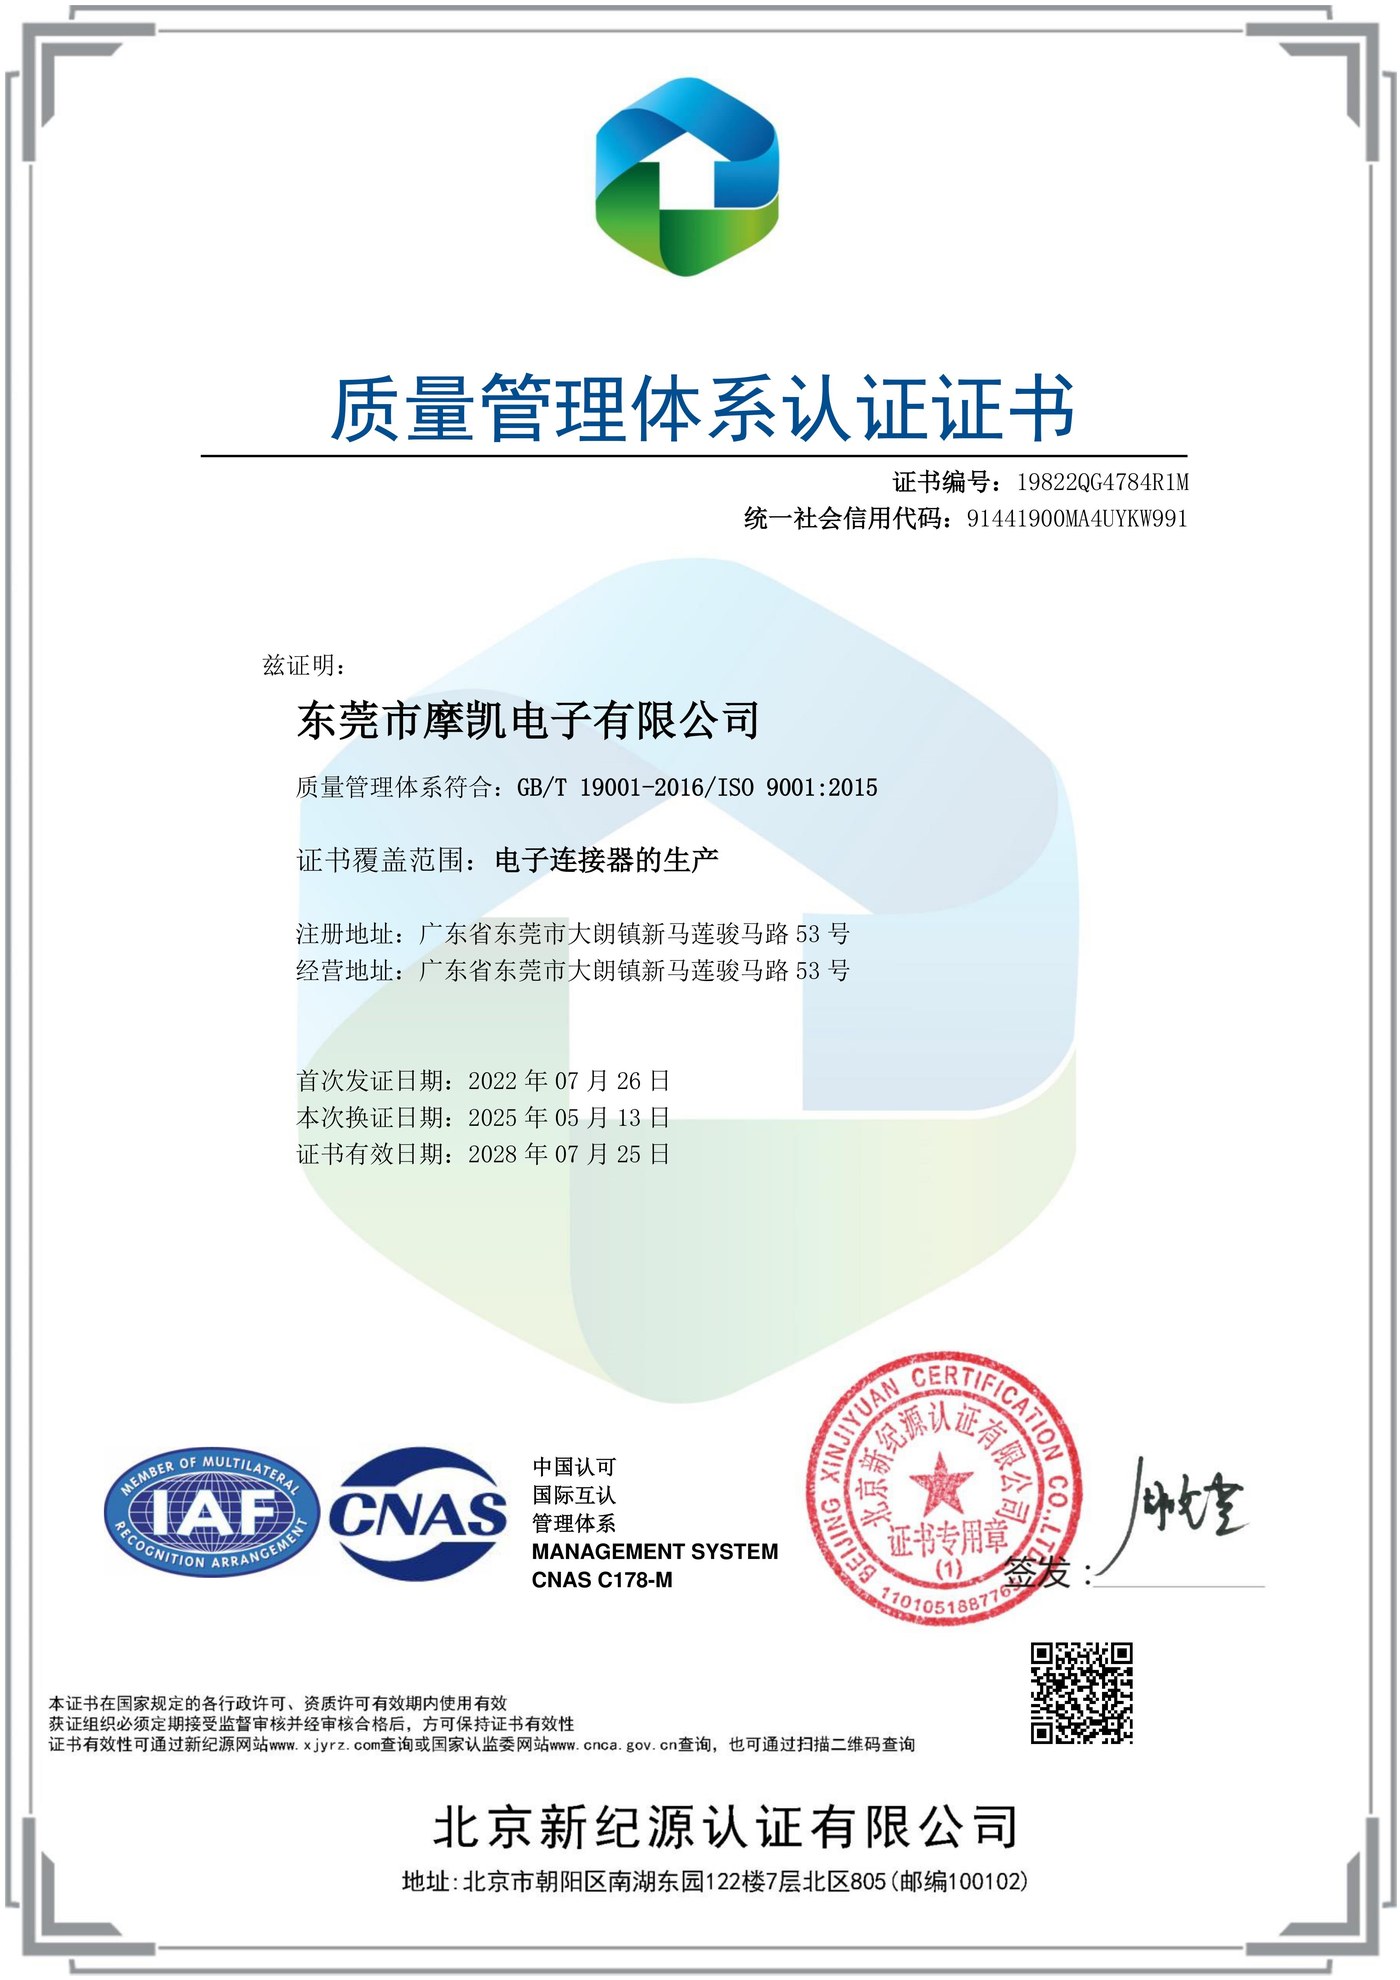
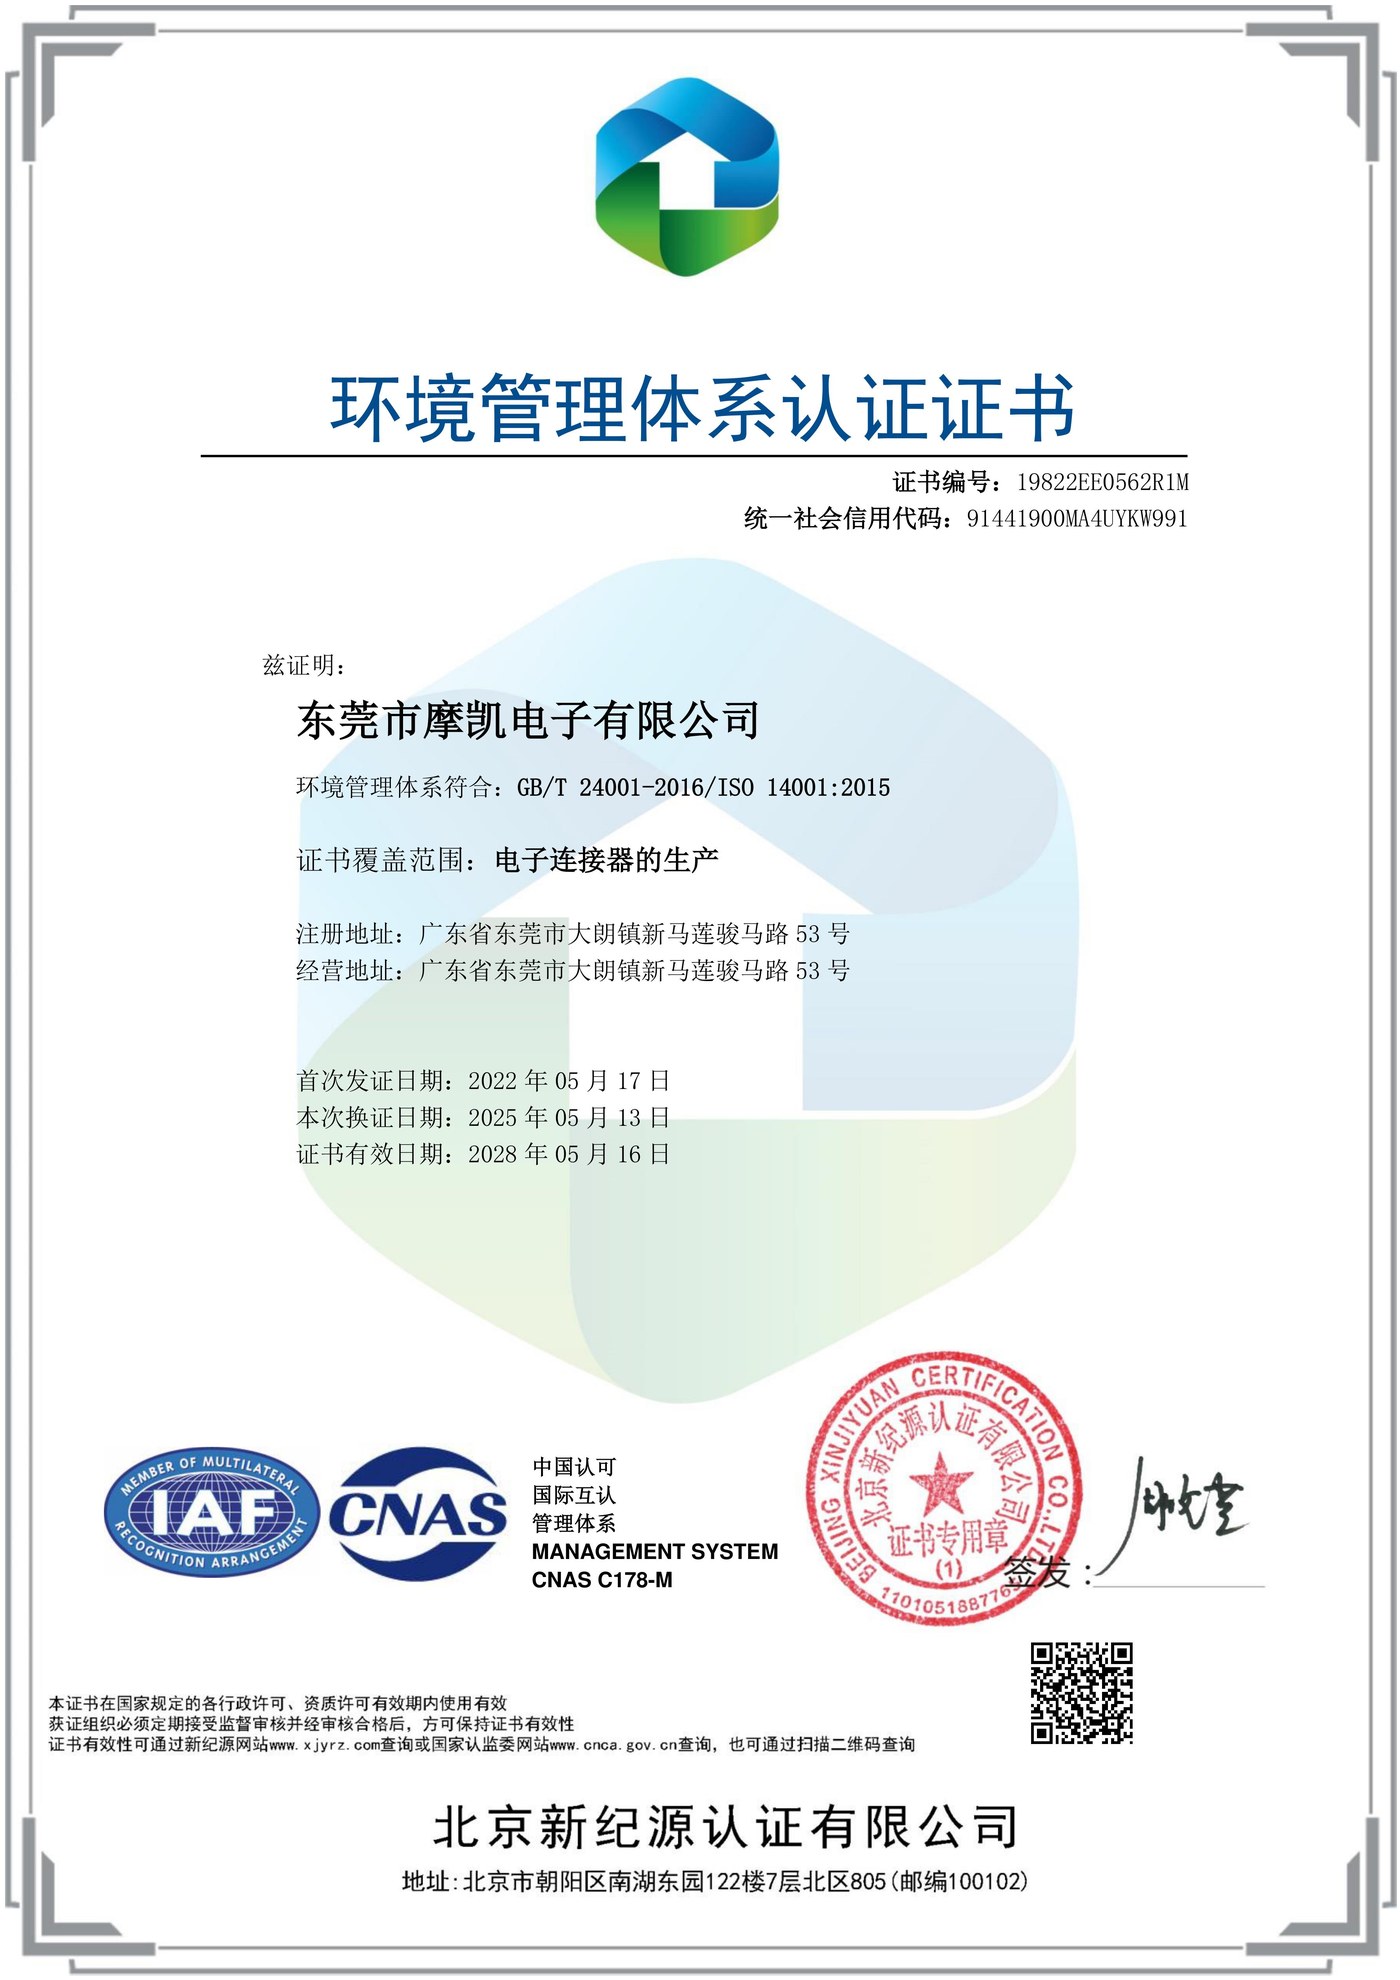
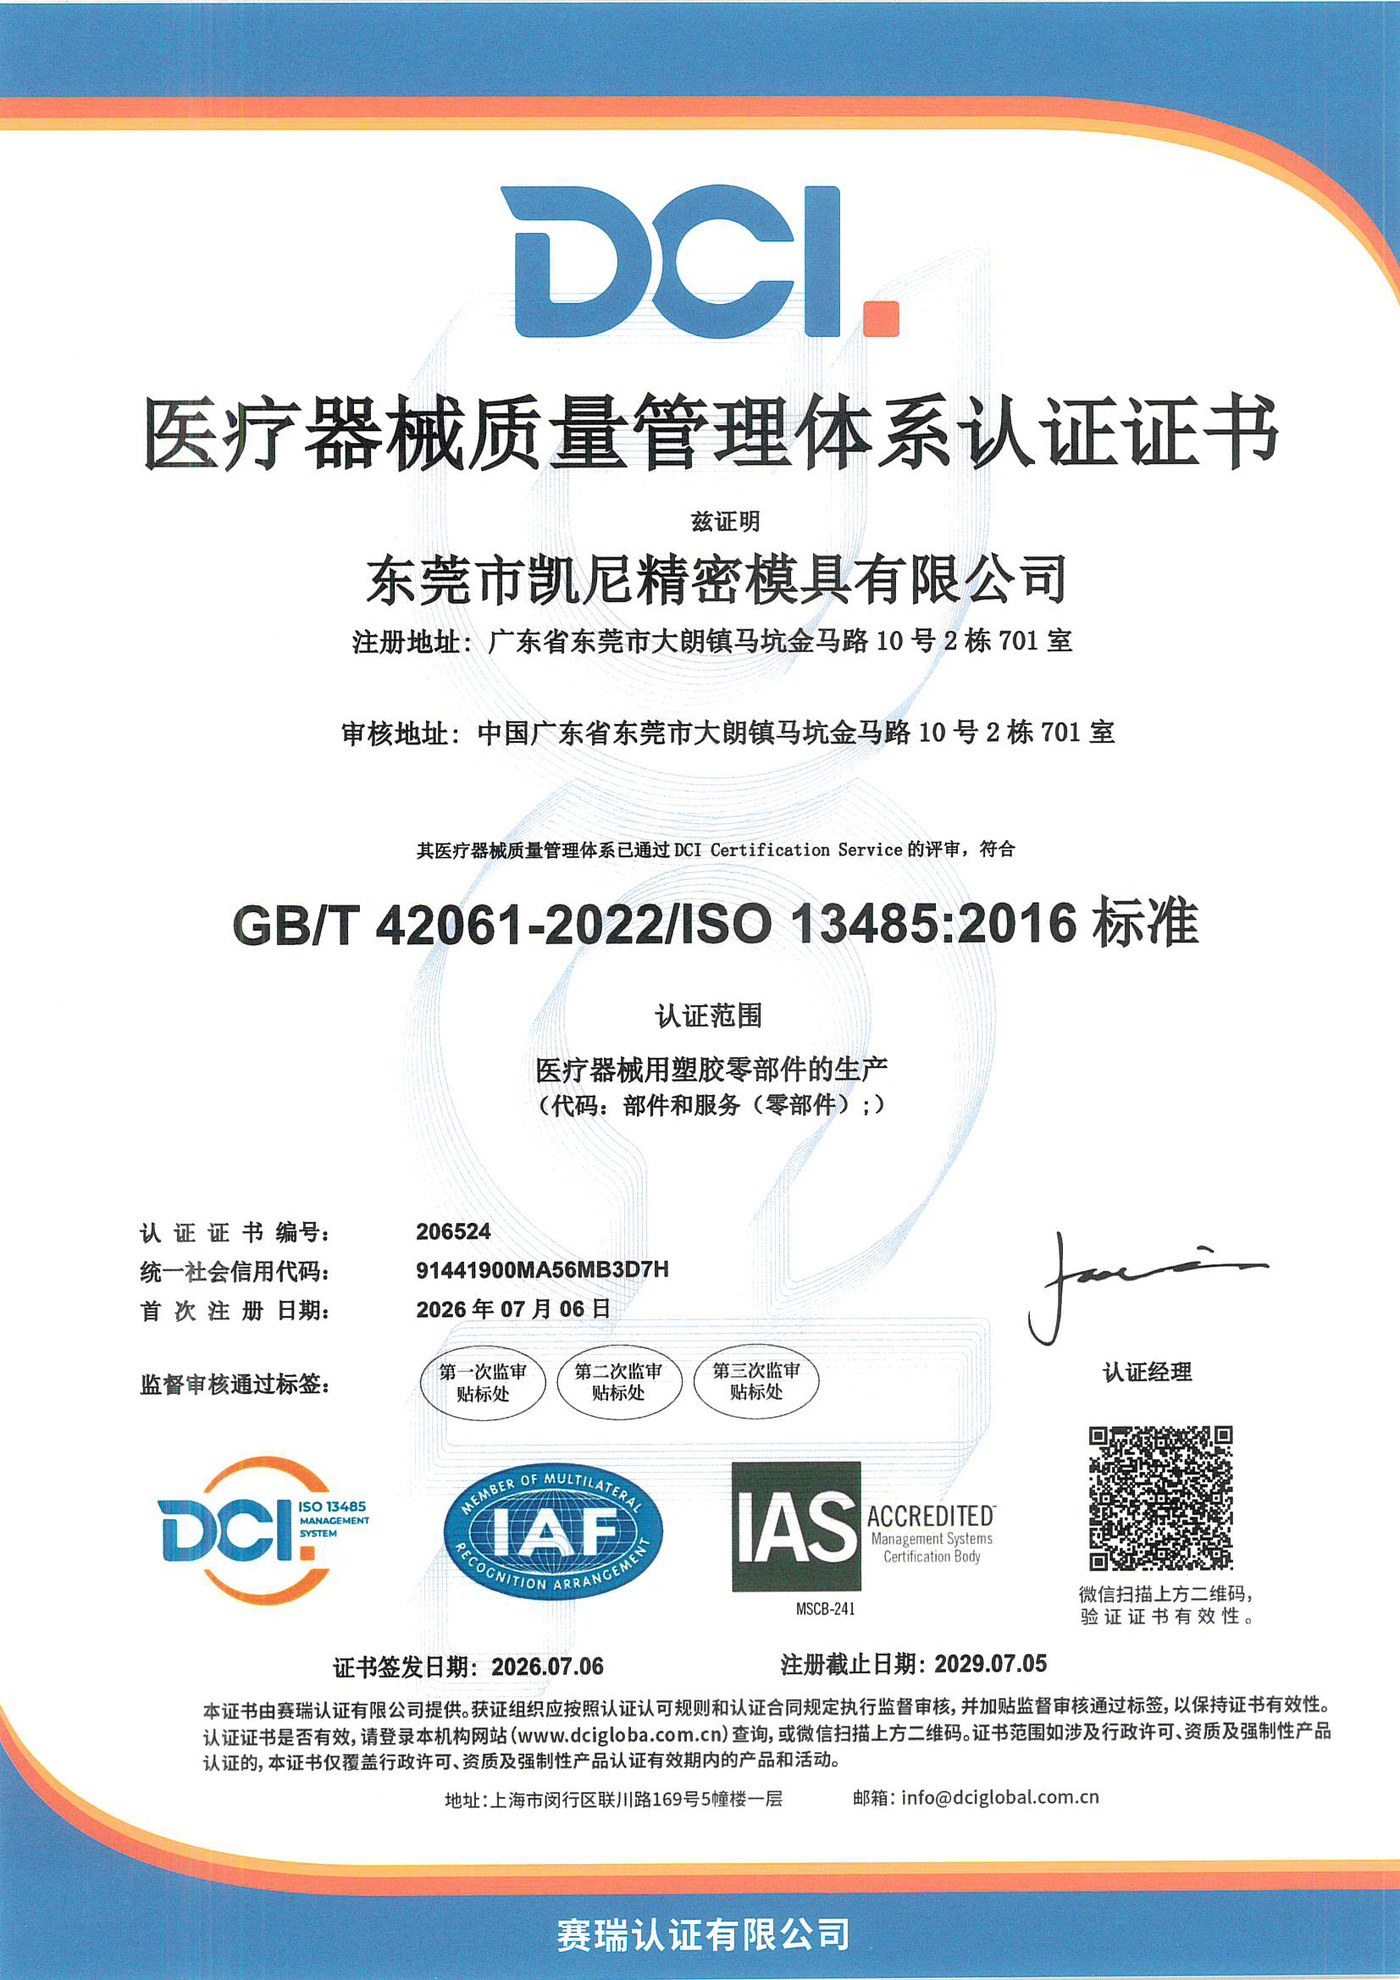
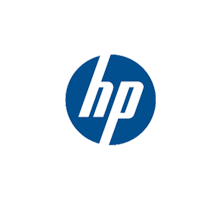
MOARCONN holds six certifications that back every card connector we ship: ISO 9001 (quality management), ISO 14001 (environmental management), IATF 16949 (automotive), ISO 13485 (medical devices, via our affiliated mold company), GB/T 31274 (restricted substances / RoHS) and National High-Tech Enterprise. Each is an independently audited credential that confirms both our product quality and the maturity of our management system. We work to one standard — every connector leaves our factory fully verified, so customers get the same dependable quality order after order.More Certificates
IATF 16949 automotive quality management system certification
ISO 9001 quality management system certification
ISO 14001 environmental management system certification
ISO 13485 medical device quality management system certification
GB/T 31274 restricted substances (RoHS) management system certification

FAQ

Frequently Asked Questions

  • 6-Pin vs 8-Pin SIM Card Connector: When Do You Need the Detect Pin?
    6-pin SIM connectors carry the essential ISO 7816 contacts for standard mobile use; 8-pin connectors add a card-detection switch for insertion check, fault reporting and hot-swap. Compare features, sizes and applications to pick the right SIM socket.
  • Who are your typical customers?
    150+ OEM/ODM manufacturing customers worldwide, serving leading terminal brands through OEM/ODM manufacturing.
  • Do you support custom card connector designs?
    Yes — OEM, ODM and self-developed modes, from drawing to mass production.
  • What is the mating cycle life of your connectors?
    10,000 mating cycles — tested to GB/T 5095.7-1997 and more than double the 3,000–5,000 cycles common in the industry.
  • Can you make ultra-thin card connectors?
    Yes — H1.15 mm and H1.1 mm in production today, from a 1.28 mm ultra-thin micro SD benchmark.
  • What certifications does MOARCONN hold?
    ISO 9001, ISO 14001, IATF 16949, ISO 13485, GB/T 31274 (RoHS) and National High-Tech Enterprise recognition.
  • How long do development and sampling take?
    A 25-day development cycle and 7-day sampling, with 24-hour FAE response.
  • What is the minimum order quantity (MOQ)?
    Zero MOQ — even one piece, with free samples and free design.
  • What is your monthly production capacity for card connectors?
    Monthly capacity of 7 million pieces and annual capacity of 80 million, backed by our own plants.
  • Do you offer exclusive territory for distributors?
    Territory, customer scope and cooperation level are agreed case by case and written into the dealer agreement before the first order.
  • What is the minimum order for a dealer first shipment?
    Standard models start at 0 MOQ, so a first shipment can be a small trial batch rather than a container load.
  • How is dealer pricing protected in the market?
    Dealers buy at direct factory price with no trading-company layer, and the agreed price level is fixed in the dealer agreement.

Quickly Customized Card Socket Connector For You

Contact us to get a quick quote and get free advice from our professional team.
Get a free quote within 2 hours

Get a free quote within 2 hours

Free design scheme within 48 hours

Free design scheme within 48 hours

From product design to initial sample within 25 days

From product design to initial sample within 25 days

  • Quick Quotation
  • For Dealer
    • *Email
      Phone
    • *Email
      Phone

Global Partners

Trust from more than 150+ partners around the world
ASUS
Dell
HP
BYD
Foxconn
Lenovo
Wistron